Friday, December 12, 2014

Cable Holder


Summary: Original design of a cable clip to keep your charging cables off of the floor. 

There are a lot of portable electronics in my house, each with its own charging cable. Whenever one of them is unplugged, the cable falls to the floor. Not only is it annoying to have to fish the cable off the floor from behind furniture, the house is starting to look like the snake pit from Indiana Jones with cables winding all over the place!

these clips from Thingiverse were way too big, 32 mm in diameter

I thought it would be easy enough to print a cable holder that would keep the cable end on top of my furniture. I tried a few designs from Thingiverse but I couldn't find any that I liked. Some were too large, others had gaps that were too wide and the cable would fall out. So I decided to make my own.

looks nice but cable slips out of gap

It turned out to be a little harder than I expected. It turns out, each charging cable had a different diameter. So if I designed a holder for a thicker cable, anything smaller would fall out. If I designed the gap for a smaller cable, I couldn't fit the thicker cables. I tried closing the gap down and making the sides thin enough to flex. That way you could bend the clip to insert the cable and the gap would close. But I was afraid the sides would crack and I didn't like the look of any of those designs.

my flexible design...meh

Finally I decided that I needed a design that snapped shut to completely enclose the cable. That way it would work with any size charging cable. Rather than go with the same hemisphere design as everyone else, I went with a cube. It took a couple of tries to get the snap feature correct; tight enough to hold together, loose enough to snap. But the final design works great. First time assembly is a little tight, but it smooths out after a few times. The orientation of the layers actually locks the halves together and keeps the pieces from sliding apart.

the Cable Box™

two halves print at same time

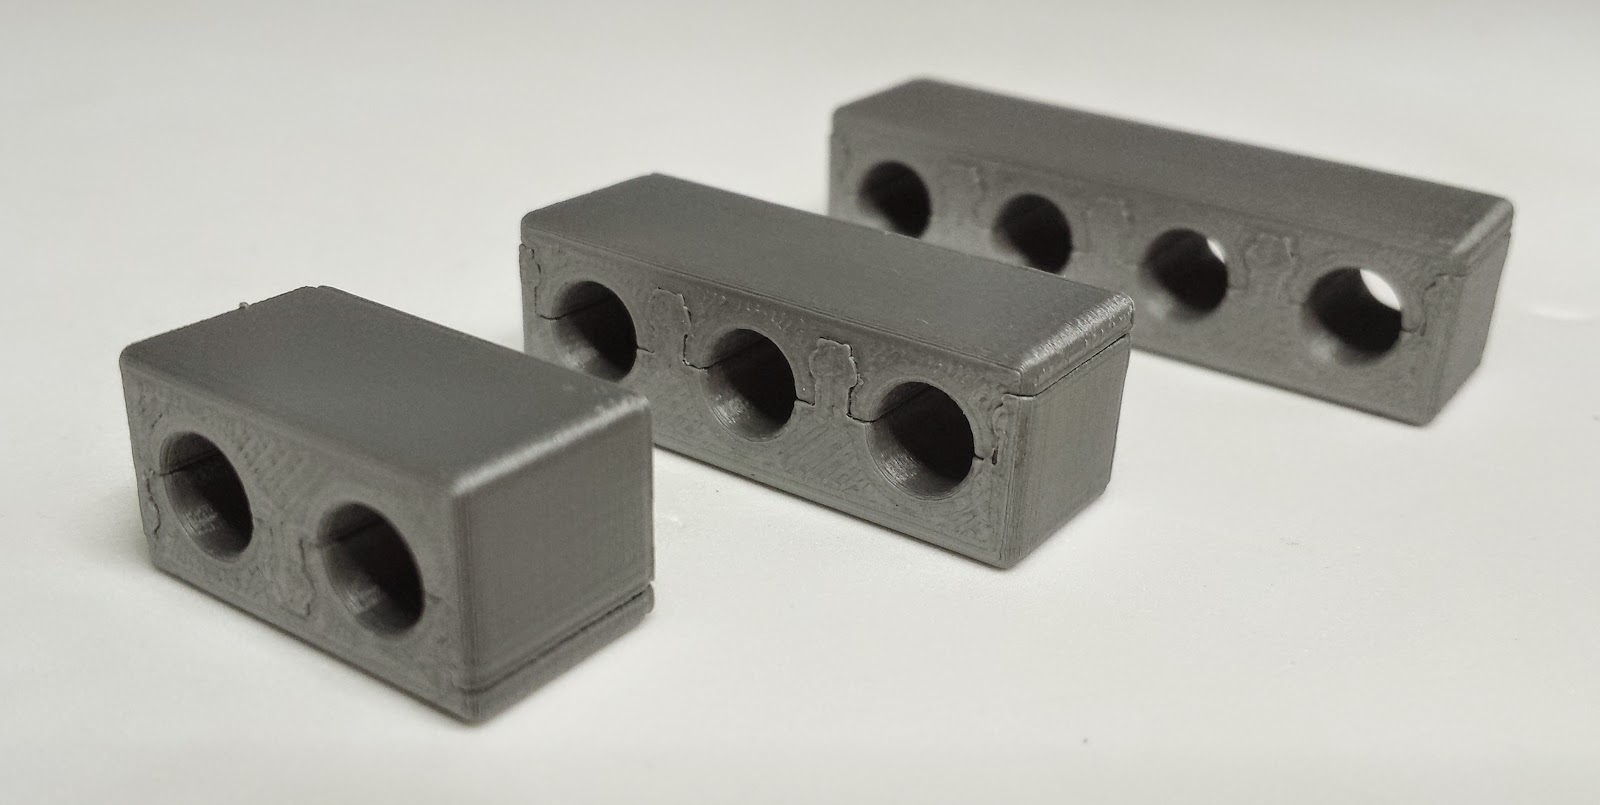
I named it the Cable Box™ after the shape. I made four versions to hold 1 to 4 cables. It is 12 mm square and has a 6 mm hole which should fit most charging cables. You attach it to surfaces with foam tape. The halves are a single .stl file but are separated on the build platform. So they print at the same time regardless of your "print one at a time" setting in Cura.


designs for 2-4 cables

Cable Box ™ in action

I printed these in PLA at 210°C with the High Quality defaults. The design works great; looks pretty good too. I'm proud of the snap-together feature. I wasn't sure I could pull that off. I'll be printing a bunch of these for my house. If you want some for your house too, the files are available on YouMagine and Thingiverse.

Wednesday, December 10, 2014

Maintenance Time!

these lines should be touching

Summary: Tighten your belts and lube the rods every 120 hours or whenever your print lines drift apart.

I just hit 120 hours of printing on my UM2. My last print was going to be a long 19+ hours. So you can imagine my despair when I noticed the first few layers weren't looking too good. There were noticeable spaces between the lines. I was printing with the normal quality defaults where the initial layers print nice and slow. It wasn't an issue of my print settings being too aggressive. The filament wasn't skipping and the lines were uniform, just not touching. So it didn't seem to be a case of under extrusion. I wasn't going to chance ruining a long print, so I aborted after just a few layers to troubleshoot.


Once again, I went to my favorite troubleshooting guide. I found the solution here. It looks like after so many hours of printing, either the belts have stretched a little, or the stepper motors have drifted in their slotted mounting holes. Luckily it is an easy fix. Simply loosen the screws for the stepper motors, apply downward pressure, and tighten the screws. Oddly enough, none of the included Allen keys fit the bolts properly (they're 2 mm). It took me longer to find the correct driver than it did to tighten the belts. While I was at it, I added a drop of silicone oil to the X and Y guide rods on the print head. Then I manually moved the print head to all extremes to distribute the oil.

initial layer after adjustments

That did the trick. Right after the maintenance, I started the print again. This time the lines were touching as expected. I was a little surprised at the improvement since the belts felt nice and tight before I adjusted them. I think Ultimaker should consider some sort of tensioner on each stepper to keep things tight. With all of the work those steppers are doing, it seems inevitable that the motors will drift some in the mounts. So just a little preventive maintenance can save you from lousy prints.

The Spiralize Setting

standard print (L) vs. spiralized print (R)

Summary: Use the "spiralize" setting for seamless walls on hollow prints like vases and cylinders.


I saw some really nice rocket models on Thingiverse. The designer recommended printing them in "vase mode". That is a mode for printing cylinders, where the table (z axis) continuously lowers as the print progresses rather than lowering in steps. That way, the print head can just go round and round without pausing when the bed lowers. It makes for seamless prints.

location of the spiralize setting

I looked in the Cura settings and couldn't find a "vase" or "continuous Z" mode. So I asked on the UM forum and found out that there is an option to "spiralize the outer contour" in the expert configurations which does the same thing. To test it out I decided to print the twin cylinder file I have been using to test print temperature. When printing in the normal Z mode, it leaves a visible vertical seam. I split the model so I could print just one cylinder. First I printed the cylinder in the normal mode. Then I repeated the print using the spiralize setting.

note the vertical seam from a standard print

inside view, spiralized print on right

The spiralize setting made nice clean cylinders with no vertical seams on the outside or inside. The internal quality is just as important when printing something you want to shine light through. Once I tested the setting on the cylinders, I printed the rocket model at .69 scale (just to save time and material). The setting worked great. I printed a little too hot and the tip of the rocket drooped a bit and there are some blobs inside the print. But there is no vertical seam. Just another great feature of Cura that you may have missed.

spiralized rocket print

lighted print

Monday, December 8, 2014

Pen Holder


I like to collect all-metal pens. I have a small collection that I would like to display on my desk rather than have them hiding in a drawer. I figured I could print a nice one but I was not able to find a design that I liked. A few days ago, I came across a design by Karas Customs on Kickstarter. I loved the look of it, but I couldn't justify the $75 price tag just to hold my pens. So I decided to draw up something similar in CAD and print it.

design in 123D Design

Drawing the holder was pretty easy. It is just a cube with 9 holes in it. But I wanted to add a custom touch, my company logo embossed on one of the sides. With my limited CAD experience, that turned out to be a bit more difficult than I expected. I am sure there are easier ways to do this, but here's how I did it.

sketching over stl object

First I opened a .png of the logo in Cura and created an .stl object just as I described in this post. Then I opened the new .stl file in 123D Design. The file had way too many faces and I couldn't manipulate the object to extrude it. So I lowered the object below the plane and manually traced a new sketch on top of it. Then I deleted the object and just saved the new sketch. Next I opened the pen holder file in 123D and inserted the new sketch.

sketch of logo with holder

Finally, I just moved the sketch into position, scaled it to fit, and extruded it into the pen holder. Then I exported the file as an .stl so I could open it in Cura and print. It sounds easy enough but it took me several tries to get the workflow correct. Again, there is probably a more efficient way to do this, but this worked for me. Like the original, I added some recesses in the bottom for rubber feet.

final design in Cura

I printed it out at the normal quality defaults. After 19+ hours, I had a really nice holder for my pen collection. It's  not as sexy as the original but I really like it and the logo adds a nice personal touch.


Sunday, December 7, 2014

Finding the Optimal Nozzle Temperature for Your Filament

proper temperature yields nice prints

Summary: Perform this easy test to find the perfect nozzle temperature for your filament.


A few days ago Doodaddoes posted this video about finding the best print temperature for your filament. I have been making test prints with the UM robot. The robot is a complicated print regardless of print temperature. It looks like the Doodaddoes method will result in clearer results because the prints are simpler.


You start with this twin cylinder file. Open the .stl in Cura using the full print settings. Change the Basic settings as below and save the G-code to your SD card. View the model in layer mode so you can be sure you do not have any top or bottom layers and your shell thickness is only a single wall. Do not use the spiralize setting, you want to see the seam of the print. It will help determine the best print.

Layer Height: 0.1 mm
Shell Thickness: 0.4 mm
Bottom/Top Thickness: 0
Fill Density: 0
Print Speed: 50 mm/s
no support, no adhesion

Make sure your filament diameter, bed temperature, fan speed, and flow are correct for your filament. Then you start printing. I start with the lowest print temperature recommended by the manufacturer. Each print takes 37 minutes at those settings.

all test prints from 190°C to 230°C (L to R) in 5°C increments

Then I print the cylinders again, each time raising the temperature 5 degrees until the print quality starts to degrade. I first tried this method with Ultimaker Ultimate Blue PLA which has a very wide recommended temperature range (190°C-260°C). I thought about printing all the way to 260°C but that would be a waste of material and risk clogging the nozzle. So I stopped once the prints started to look bad. To test the prints I first look for signs of under extrusion and check the surface finish. Then I try to pull the layers apart by putting my pointer fingers in each side, grasping with my thumbs, and pulling in line with the cylinder. Finally, I squeeze the sides of the print together to see if it cracks or the layers split.

under extrusion and weak layer bonding at 190°C

messy seam at 225°C

rough surface finish at 230°C

You can see evidence of under extrusion at 190°C-200°C. The bonding between the layers was also very weak and easy to pull apart. The 205°C and 210°C prints look great with the seam being just a little cleaner on the 210°C print. Layer bonding was nice and strong and the print held up when squeezed together. At 215°C gaps started to appear in the seam and got worse at each increase in temperature after that. At 220°C the layers became more obvious and by 225°C there was significant stratification of the layers. And by 230°C the surface finish of the print became very rough. There wasn't any point in printing at any temperature beyond that. It looks like 210°C is the perfect temperature for Ultimate Blue PLA on my machine.

great layers at 200°C

I repeated the test with MatterHackers Pro Series green PLA. There was under extrusion at 185°C to 195°C. The prints were perfect at 200°C. Although the recommended temperature range is only 185°C to 200°C,  I printed at 205°C and 210°C as well. Those prints were very good but the seam was cleaner and the surface finish was just slightly better at 200°C.

This is a terrific way to find the best print temperature for your filament. The prints are relatively quick and the differences in print quality are easy to see. I will be performing this test first with every new batch of filament I buy.

Friday, November 28, 2014

First Prints in ABS

ABS print

Summary: Printing in ABS is easy. Lower default nozzle temperature for best print quality.

I have a number of parts to make for my custom hexacopter. I needed to print them in something tougher than PLA that can hold up to some hard landings and withstand high temperatures like in a car. So I ordered some Pro Series ABS filament from MatterHackers. If you read up on printing with ABS you can easily psyche yourself out. So much advice on getting successful prints with ABS. I chose to ignore all of it and just print the Ultimaker Robot with the default ABS settings at normal quality.

normal quality print at 260 C

The default ABS settings are 260°C nozzle, 90°C bed, 50% fan, 2.85 mm filament diameter and 107% flow. I used glue on the bed to help the part stick. The part printed without any problem and stuck to the platform firmly. Print quality was pretty good but it looked like it printed a little hot. The color also looked to go a little light and matte compared to the bright gloss red of the filament. The first few layers printed a little messy with nubs of material, same for some of the infill. The small details like the antennae and ears looked melted and the bridges looked bad. The Pro Series ABS is rated for 230°C - 240°C so I decided to print again at 240°C. This time I adjusted the filament diameter to 2.90 mm.

260C print (L) vs 240C print (R)

This 240°C print turned out a little better. The initial layers printed clean as did the infill. The color of the part also got brighter. The fine details printed much better and the bridges improved slightly. On another note, many people complain about the smell of ABS during printing. While it does have a faint smell of melting plastic, I found it underwhelming. It was only really noticeable when close to the printer; not a problem. Let's try one more print at 230°C.

240C print (L) vs 230C print (R)

At 230°C the small details and bridges improved a little more. Most noticeable, the sides of the print were smoother. At this point, the ABS prints nearly as well as PLA. Larger prints may not be so easy, bed adhesion and warping may become an issue, we'll see. But for now I'm ready to make some parts in ABS.

ABS (L) vs PLA (R) prints

Tuesday, November 25, 2014

Separating Parts in Cura

all parts are one object

Summary: Separate multi-object files into separate parts for easier printing.

I am working on a multi-part model. One of the stl files contains several parts. When the file is imported into Cura, they are seen as a single object. This was a problem because some of the pieces needed to be rotated. Luckily this is easy to fix in Cura. Simply right click on the model and select "split object into parts".

model split into 11 objects

In a matter of seconds, Cura splits the model into multiple parts. Each part can now be repositioned and rotated as needed. Or, you can save each of the parts as a separate stl file by copying the file and deleting the unwanted parts. This is just one of those handy options in Cura that is easy to miss.